
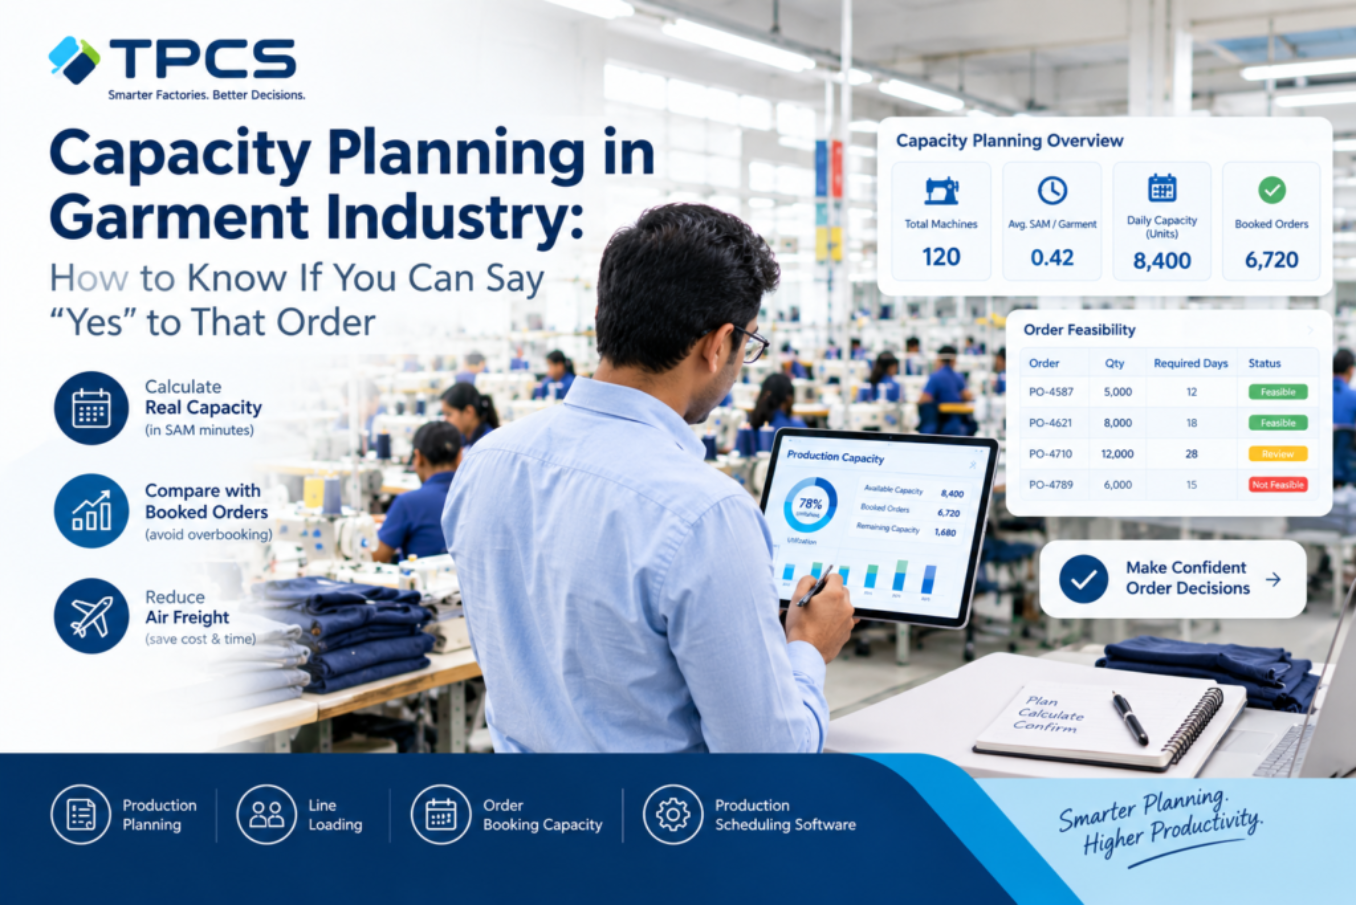
Garment factory capacity is best measured in SAM (standard allowed minutes), not pieces. Monthly capacity = Number of operators × Working minutes per day × Working days × Expected efficiency. To check whether you can accept an order, multiply order quantity by style SMV and compare the result with the capacity still free in that delivery window, line by line.
The October that cost ₹18 lakh in air freight
This is a composite scenario drawn from situations we see often in Indian factories.
Farhan runs an export house in Okhla, Delhi, with eight sewing lines. In August, a European buyer offered a 40,000-piece order of women’s dresses for November delivery. Good price, good buyer. His merchandising team checked the calendar, saw that lines were “mostly free” in October, and said yes.
What nobody calculated was minutes. October already had three running orders. Diwali shut the factory for several days. After Chhath, a good share of operators from Bihar and eastern UP came back a week later than planned. And the new dress style was more complex than anything those lines had stitched that year.
By mid-November, the factory was 12 days behind. The buyer agreed to keep the order, but only if the balance shipped by air. The air freight bill was close to ₹18 lakh, almost the entire margin on the order.
Farhan didn’t lack lines. He lacked a way to see capacity in the same unit as the orders: minutes.
Why “pieces” is the wrong unit for capacity
A line that makes 800 T-shirts a day might make only 250 blazers. Pieces don’t travel across styles. Minutes do. That’s why planners convert everything into SAM minutes:
- Capacity = minutes your people can produce
- Load = minutes your orders need (quantity × style SMV)
When load exceeds capacity in any week, you have a problem, no matter how “free” the line looks on a wall chart.
Step 1: Calculate available capacity
Monthly capacity (SAM minutes) = Operators × Minutes per day × Working days × Efficiency
Worked example for Farhan’s factory:
- 8 lines × 35 operators = 280 operators
- Shift of 8.5 hours = 510 minutes
- 26 working days
- Average efficiency 55%
280 × 510 × 26 × 0.55 = 20,42,040 SAM minutes per month
Be honest about the inputs. Use present operators (after typical absenteeism), not headcount on the muster roll. Remove festival holidays, planned shutdowns and buyer audit days. Use your actual average efficiency, not your best week.
Step 2: Calculate load from booked orders
Load = Order quantity × Style SMV
| Order | Quantity | SMV | Load (minutes) |
|---|---|---|---|
| Existing orders (3 styles) | — | — | 14,50,000 |
| New dress order | 40,000 | 22.0 | 8,80,000 |
| Total load | 23,30,000 |
Step 3: Compare load with capacity
23,30,000 ÷ 20,42,040 = 114%
The factory was overbooked by about 2,88,000 minutes, or 14%, before a single festival or migration delay was considered. With those included, the gap was bigger.
Had Farhan seen this in August, he had real options: negotiate a split delivery, outsource part of the order to a trusted job-work unit, add a Sunday shift with overtime paid at the legally required rate, or decline politely and protect the relationship.
Step 4: Account for the learning curve
A new style never starts at full efficiency. A line might begin at 25–30% on day one and climb over 7–10 days. For complex styles, the climb takes longer. If you plan a new style at the line’s average efficiency from day one, you’ll be behind before you start.
A simple approach: plan the first week of any new style at roughly half your mature efficiency and increase gradually.
Step 5: Load lines, not the factory
Factory-level capacity tells you whether to accept an order. Line-level loading tells you whether you can deliver it. Not every line can make every product. A line set up for knit tops may struggle with tailored woven dresses.
Good line loading considers:
- Product suitability: machine types and operator skills on each line
- Material readiness: fabric and trims in-house before the planned start date (link this to your TNA)
- Changeover loss: every style change costs output for a few hours or days
- Delivery sequence: earliest ex-factory dates first, unless a buyer has penalties that change priorities
India-specific capacity killers to plan for
- Festival season: Diwali, Durga Puja, Pongal, Eid and Chhath affect attendance differently by region and by workforce mix.
- Migrant workforce return lag: many units see attendance dip for one to two weeks after major festivals.
- Monsoon: waterlogging and power cuts in some industrial areas.
- Peak-season overtime: under the new Labour Codes, overtime requires worker consent and is paid at double the ordinary rate, so overtime is a costly, not free, buffer.
- Buyer audits and inspections: they take supervisors and lines off production for hours.
A simple capacity review routine
- Every Monday, update next 12 weeks of capacity (operators, days, efficiency).
- Update load from all confirmed and likely orders.
- Highlight any week where load exceeds 90% of capacity.
- Before confirming a new order, check load in its delivery window, line by line.
- Review material readiness for the next four weeks of planned starts.
Where software helps
A spreadsheet can do Step 1 to Step 3 for one factory with a few orders. It falls apart when orders change daily, efficiency shifts and fabric arrives late. TPCS handles this through:
- Capacity calendar: SAM-based capacity by line, by week, with holidays and shift changes built in.
- Production planning: drag orders onto lines and see load vs capacity instantly.
- TNA integration: planned start dates linked to fabric and trims readiness.
- Live efficiency from MES: capacity updates based on actual line performance, not assumptions.
How Farhan’s story ended
Farhan now runs a Monday planning meeting with a single screen: a 12-week load-versus-capacity chart by line. Merchandisers can’t confirm an order without checking it. The following festive season, the factory turned down one order, split another into two deliveries and shipped everything by sea.
Frequently asked questions
How do you calculate garment factory capacity?
Monthly capacity in SAM minutes = Operators × Working minutes per day × Working days × Efficiency. For example, 280 × 510 × 26 × 0.55 = 20,42,040 minutes.
What is the difference between capacity planning and production planning?
Capacity planning checks whether you have enough minutes to accept orders. Production planning decides which line makes which order, in what sequence and on which dates.
What is line loading in the garment industry?
Line loading is assigning specific orders to specific sewing lines based on product suitability, material readiness and delivery dates.
How do festival holidays affect garment production planning in India?
They reduce working days and often reduce attendance for one to two weeks after major festivals, especially in units with a large migrant workforce. Plan lower capacity for these weeks rather than hoping for overtime.
Which software is used for production planning in garment factories?
Apparel-specific MES or ERP systems with capacity calendars, line loading and TNA, such as TPCS, are built for this, as they plan in SAM minutes and handle style-level SMV.
See your next 12 weeks before you say “yes”
Book a TPCS demo and we’ll set up a capacity-versus-load view using your lines, your holidays and your current orders.